Fusion Splicing Problems: Bubbles, Separation, Thin and Fat Splices Explained

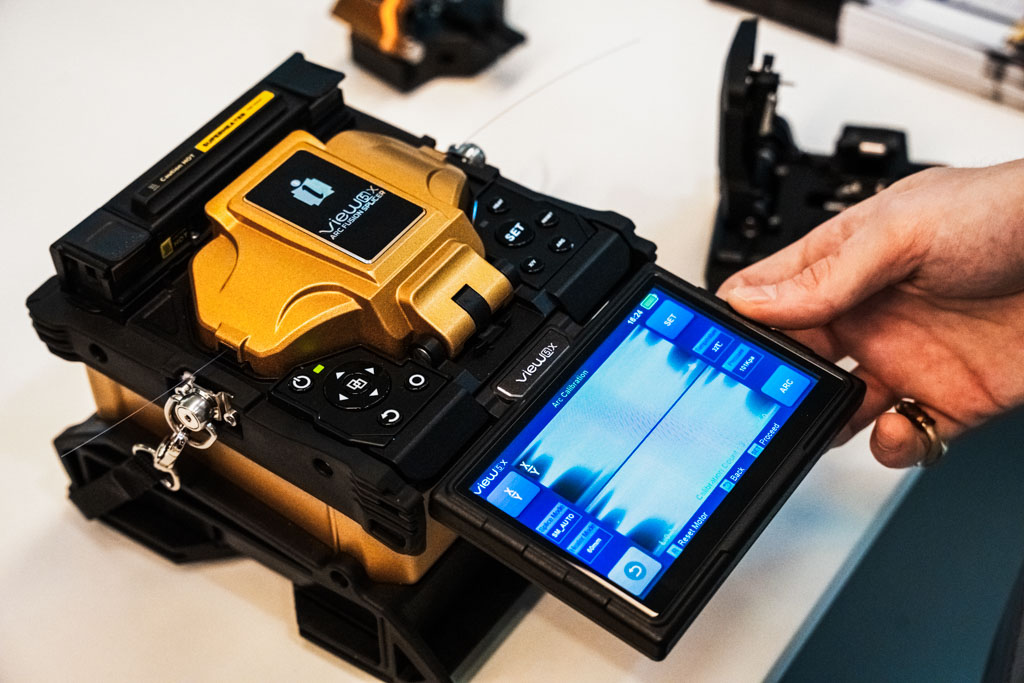
Every splicing technician sees error messages sooner or later, whatever their level of experience. Most fusion splicing problems do not mean the splicer is faulty. The splicer is telling you that something in the preparation, the environment or the arc settings needs a small adjustment. Once you know how to read those messages, most of them take seconds to fix.
This guide covers the four splice defects we are asked about most often at our UK service centre. For each one we explain what you will see on screen, why it happens and how to prevent it. At the end you will find a short checklist for deciding when a problem can be solved in the field and when it is quicker to send the splicer to us.
Start with the basics: arc calibration and a clean splicer
Many fusion splicing problems can be avoided before the first splice of the day. The single most useful habit is to run an arc calibration whenever your working conditions change. Temperature, humidity, altitude and even moving from a warm van to a cold chamber all change how the arc behaves. Arc calibration lets the splicer measure those conditions and adjust arc power automatically.
In the UK that matters more than people expect. A morning that starts at 3°C in a damp footway box and ends at 18°C in a cabinet is a different environment for the arc, and a splicer calibrated at the depot will not be ideally set for both.
Alongside calibration, check these three things as part of routine preparation rather than only when something goes wrong:
- the condition and arc count of the electrodes
- the cleanliness of the V-grooves and fibre clamps
- the condition and position of the cleaver blade
Modern INNO fusion splicers also check the fibres before the arc fires. If you see a message such as Right fiber core dirty, the splicer has stopped you from making a high-loss splice. Re-clean or re-cleave the fibre and carry on.
Bubble at the splice point
After the splice, the screen shows a small dot or bubble exactly where the two fibres were joined. The fibres look fused, but there is a visible imperfection in the joint.
Why it happens
A bubble forms when gas or contamination is trapped in the molten glass. The usual causes are:
- dust, gel or coating residue on the fibre surface
- a poor or chipped cleave
- pre-fuse time that is too short for gases to escape
- unstable arc conditions after a change in environment
How to prevent it
- Clean each fibre with lint-free wipes and high-purity isopropyl alcohol after stripping.
- Check the cleave angle on screen and inspect the cleaver blade if poor cleaves keep appearing.
- Allow enough pre-fuse time, particularly in cold or damp conditions.
- Run an arc calibration whenever conditions change.
- Keep the electrodes and V-grooves clean.
Separation
The splicer reports separation. On the image you may see a gap or a weak neck at the splice point, and sometimes the fibres look aligned but are not properly joined.
Why it happens
Separation means the fibre ends did not bond during the arc. Instead of merging, the molten glass pulls back. This is often linked to:
- not enough glass at the joint, usually from an incorrect stripping or cleave length
- arc power that is too strong or unstable
- a pre-fuse time that is too long and rounds off the fibre ends
- a change in environment since the last calibration
How to prevent it
- Use the correct stripping and cleave length for your splicer and fibre holders.
- Make sure both fibres sit firmly in the holders and V-grooves.
- Avoid unusually long pre-fuse settings.
- Run an arc calibration and check the electrode arc count.
Splice too thin
The splicer reports too thin and the image shows a narrowed section at the joint. The fibre diameter at the splice point is visibly smaller than the fibre either side.
Why it happens
A thin splice is caused by the molten glass being overheated or stretched. Common reasons are:
- arc power set too high for the conditions
- too little fibre at the joint because of a short stripping length
- misalignment during fusion
- arcing the same splice several times
A thin splice is weaker mechanically and usually shows higher loss, so it is worth remaking rather than protecting.
How to prevent it
- Run an arc calibration after any change in temperature, humidity or location.
- Prepare fibres to the correct stripping length.
- Cut out and remake a poor splice instead of re-arcing it repeatedly.
- Keep the V-grooves and alignment area clean.
Splice too fat
The splicer flags the splice as too fat, and the joint looks thicker than the surrounding fibre. The splice may look solid, but the uneven shape disturbs the light path and adds loss.
Why it happens
- too much fibre pushed into the joint
- arc duration that is too long
- fibres not properly centred before fusion
- arc settings that do not suit the environment
How to prevent it
- Keep stripping and cleave lengths consistent.
- Avoid extending arc time unless the fibre type needs it.
- Check fibre centring on screen before you start the splice.
- Calibrate the arc and make sure the electrodes are clean and within their arc count.
Quick reference: symptoms and first checks
| What you see | Most likely cause | First thing to check |
|---|---|---|
| Bubble | Contamination or poor cleave | Fibre cleaning and cleave quality |
| Separation | Too little glass or unstable arc | Stripping length and arc calibration |
| Too thin | Arc too strong or fibre stretched | Arc calibration and stripping length |
| Too fat | Too much fibre or arc too long | Cleave length and fibre centring |
| Repeated core or end-face errors | Worn cleaver blade | Blade position and blade height |
When to stop troubleshooting and book a service
Most errors disappear once the fibre preparation, electrodes and arc calibration are right. If they keep coming back, the cause is more likely to be inside the splicer. Book a service if you notice any of the following:
- errors continue after fresh electrodes, a new cleave and a successful arc calibration
- arc calibration fails or gives very different results each time
- the camera image is blurred, dark or has fixed spots that do not clean away
- the motors make unusual noises or the fibres do not move smoothly
- the splicer has been dropped, got wet or has not been serviced for more than a year
Our fusion splicer service and repair centre in the UK handles INNO splicers and cleavers for customers across the UK and Ireland, with a 3-working-day turnaround. If you are not sure whether the problem is the device or the technique, send a photo of the splicer screen to our support team. It is often enough for us to point you to the fix straight away.
Keep your kit in good order
Good splices depend as much on consumables as on the splicer itself. We hold replacement electrodes, cleaver blades and fibre cleavers in UK stock, and orders are dispatched the same or next working day. For more detail on the parts that cause most errors, read our guides on when to replace fusion splicer electrodes and cleave quality and blade care. If you work with mixed fibre types, choosing the right splice mode is the next thing to check.
Need help now? Contact our UK support team and we will get back to you quickly.